A compressed air system can have well-maintained compressors and still waste significant energy if they are operating in the wrong order. Learning how to optimize compressor sequencing helps plants match air supply to actual demand, reduce unloaded run time, stabilize system pressure, and protect production from avoidable outages.
For facilities with multiple compressors, sequencing is not simply a matter of turning on the next available machine. Each compressor has a different capacity, control method, operating cost, and maintenance condition. The sequence must account for how the plant uses air throughout the day, not just the total horsepower installed.
Start With the Demand Profile, Not the Compressor Room
The best compressor sequence begins with a clear picture of demand. Many plants know their installed compressor capacity but do not know how much air the process actually needs by shift, production line, or operating state.
Measure airflow and pressure over a representative period. Include normal production, peak production, weekends, shift changes, cleaning cycles, and low-demand periods. A single high-demand event should not dictate how the system operates for the remaining 95 percent of the week.
Look for recurring patterns. If demand sits around 600 cfm most of the day but briefly rises to 1,000 cfm during changeovers, the system should efficiently cover the 600 cfm base load while bringing on additional capacity only when needed. Running large compressors unloaded to cover short peaks is often expensive and hard on equipment.
Pressure trends matter just as much as airflow. A system that repeatedly drops pressure before another compressor starts may have sequencing delays, inadequate storage, a poorly positioned pressure sensor, restrictions in piping, or leakage. Adding another compressor without identifying the cause can increase power consumption without solving the production issue.
Assign Base, Trim, and Standby Roles
Once demand is understood, each compressor should have a defined job. In most multi-compressor systems, that means assigning base-load, trim, and standby roles.
A base-load compressor handles the steady portion of demand. It is usually the machine with the best energy performance at full load and the capacity that most closely fits the plant's consistent air requirement. Fixed-speed rotary screw compressors often work well in this role when they can remain heavily loaded.
A trim compressor responds to changing demand. A variable speed drive compressor can be effective as trim when demand varies frequently, because it can adjust output rather than repeatedly loading and unloading. That does not mean a VSD compressor is automatically the best trim choice in every installation. Its operating range, minimum stable capacity, turndown, control response, and maintenance requirements all need to fit the system.
Standby capacity is different from trim capacity. A standby machine should be ready to support peak demand, cover maintenance, or protect critical operations when a lead compressor fails. In a hospital, defense operation, municipal facility, or production environment where air loss stops the process, standby planning is an uptime decision, not excess capacity.
How to Optimize Compressor Sequencing With Controls
Compressor controls determine when each machine loads, unloads, starts, stops, or changes speed. Poorly coordinated local controls can make several compressors fight each other. One machine unloads while another starts, pressure swings widen, and total power rises.
For systems with two compressors and relatively stable demand, properly set local controls may be sufficient. The lead compressor should carry the base load, while the second machine starts only after pressure and demand conditions justify it. Pressure bands must be coordinated so the machines do not overlap unnecessarily.
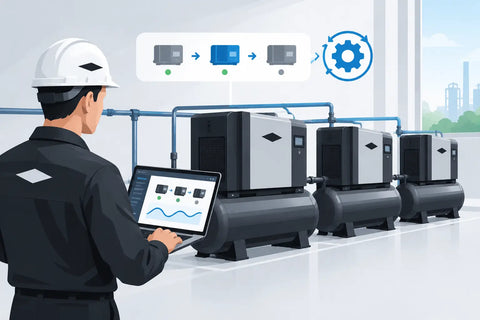
As systems grow, a central sequencing controller usually provides better results. A master controller can monitor system pressure and demand, choose the most efficient combination of available compressors, rotate runtime, and account for service status. It can also prevent a lightly loaded machine from remaining online when a different compressor combination would use less power.
The controller should not be configured solely around nameplate horsepower. It needs current performance information. A 200 hp compressor that has lost capacity, runs hot, or has a control issue may no longer be the right base-load unit. Likewise, a compressor scheduled for service should not remain the default lead machine just because it is first in the programmed sequence.
When configuring controls, establish realistic setpoints. Excessive pressure is costly. Every additional pressure increase requires more compressor energy, while leaks and inappropriate end uses tend to consume more air at higher pressure. The goal is to run at the lowest stable pressure that supports the most demanding legitimate process requirement.
Avoid the Most Common Sequencing Mistakes
The first mistake is using pressure alone as the whole strategy. Pressure is an essential control signal, but it reacts after demand changes. If storage is too limited or the pressure sensing point is poorly selected, control decisions may be late and unstable.
The second is relying on wide pressure bands to stop frequent cycling. Wide bands may reduce starts and stops, but they can create pressure variation that affects tools, valves, instrumentation, and product quality. Storage and better controls are often more effective than accepting large pressure swings.
The third is setting every compressor to the same pressure range. When machines have overlapping setpoints, they may all load together, then unload together. This creates inefficient operation and makes it difficult to identify which machine is truly carrying the base load.
The fourth is overlooking air storage. Wet storage near the compressors provides a reserve that helps manage changing demand. Dry storage near intermittent high-demand equipment can reduce sudden pressure drops at the point of use. The right storage arrangement depends on compressor type, dryer configuration, demand events, and process sensitivity.
Finally, do not treat leaks as a separate issue from sequencing. Leaks raise the base load, which may force an additional compressor online for no productive reason. Before changing sequence logic, identify major leaks, artificial demand, undersized piping, and inappropriate uses of compressed air.
Match the Sequence to Real Operating Scenarios
A sequencing plan should be tested against real plant conditions, not only modeled at average demand. Review what happens during startup, shift changes, production surges, emergency operation, and planned maintenance.
For example, a plant with one 150 hp fixed-speed compressor, one 100 hp fixed-speed compressor, and one 100 hp VSD compressor may use the 150 hp unit as the base-load machine during full production. The VSD can trim normal fluctuations, while the second 100 hp unit remains available for larger peaks or redundancy.
During nights or weekends, that same sequence may be inefficient. If demand drops below the efficient operating range of the 150 hp machine, the VSD compressor alone may carry the reduced load more effectively. The lead assignment should change by schedule or demand condition when the operating profile supports it.
This is why a sequencing strategy should be reviewed after major production changes. A new line, expanded shift schedule, changed packaging equipment, or additional pneumatic tools can alter demand enough to make an old control setup inefficient.
Use Maintenance Data to Keep the Sequence Reliable
Sequencing only works when compressors deliver their expected capacity. Dirty coolers, restricted filters, failed drains, worn inlet valves, oil carryover, belt issues, and neglected service intervals can all reduce performance or create unstable operation.
Track operating hours, loaded hours, unloaded hours, starts, discharge temperature, pressure, power draw, and maintenance alarms for each compressor. These trends help identify whether a sequencing issue is actually a mechanical or maintenance issue.
Runtime rotation is also valuable. Rotating lead duty spreads wear across available compressors and prevents a backup machine from sitting idle for long periods. However, rotation should not override efficiency. A less efficient compressor may need to run periodically for readiness, but it does not have to be the primary base-load machine during the most energy-intensive production hours.
Certified technicians can verify compressor performance, evaluate control logic, inspect storage and piping, and identify the practical improvements that produce measurable results. For facilities in Southern California and Arizona, Advanced Air & Vacuum can support a complete system review, from equipment condition and controls to installation and preventative maintenance planning.
Verify Results After Every Adjustment
Do not assume a new sequence is better because the pressure looks stable. Confirm the change with data. Compare energy use, pressure stability, compressor runtime, unloaded operation, production interruptions, and maintenance alerts before and after the adjustment.
A useful benchmark is specific power: the kilowatts required to produce 100 cfm of air. If the system produces the same useful airflow with lower specific power and stable pressure, the sequence is moving in the right direction. If power falls but pressure problems or production complaints increase, the settings need refinement.
The most effective sequencing plan is rarely permanent. It is a controlled operating strategy that changes with demand, equipment condition, and production priorities. Start with accurate data, assign clear compressor roles, and keep the system maintained so every machine can perform when the plant needs it most.
